
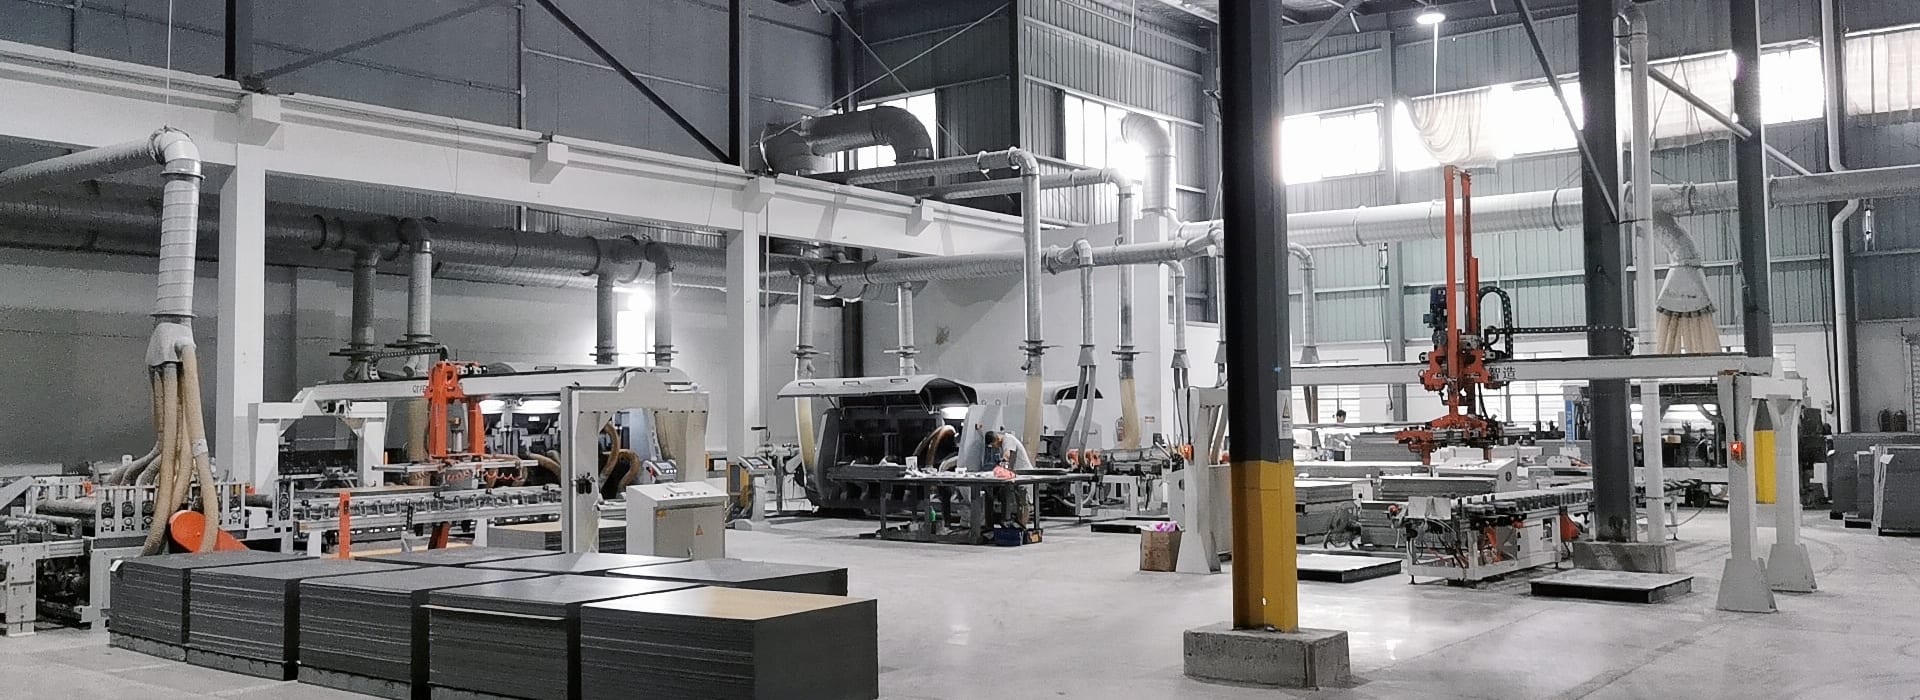
Manufacturing
Production & Quality
From raw material to finished product — how we manufacture and how we control quality at every stage.
Virtual Factory Tour
Follow the journey of every MGT® plank — from raw limestone and PVC powder to inspected, packed flooring ready for export.
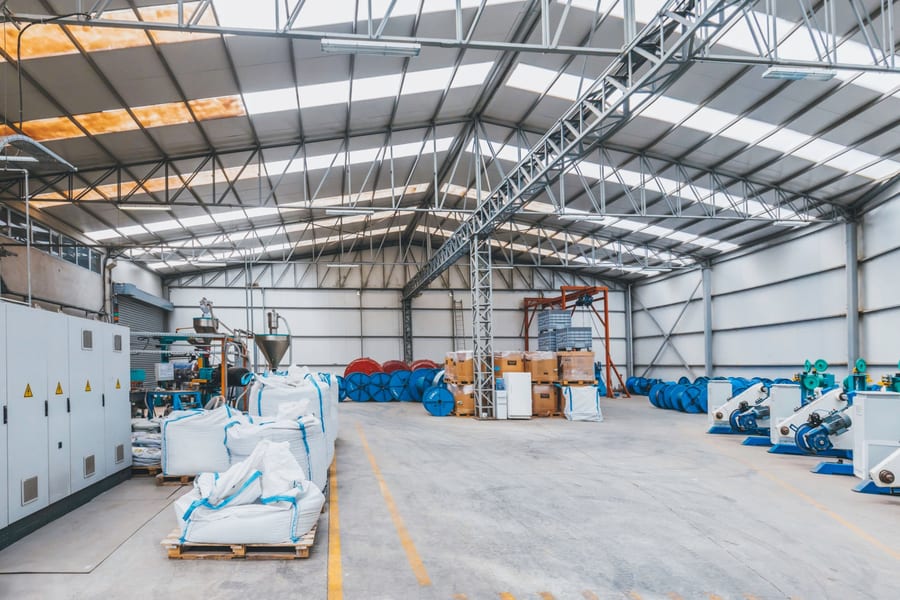
Raw Material Intake
Virgin PVC powder, limestone filler (CaCO₃), stabilizers, and processing aids are received from qualified suppliers and stored in dedicated silos and warehouses. Before release to production, every incoming batch is tested for key parameters such as particle size, moisture content, and bulk density. Materials that do not meet the specification are rejected and returned to the supplier. Strict FIFO rotation ensures older stock is used first, so material freshness and traceability are maintained from the moment it enters the factory to the moment it reaches the mixing line.
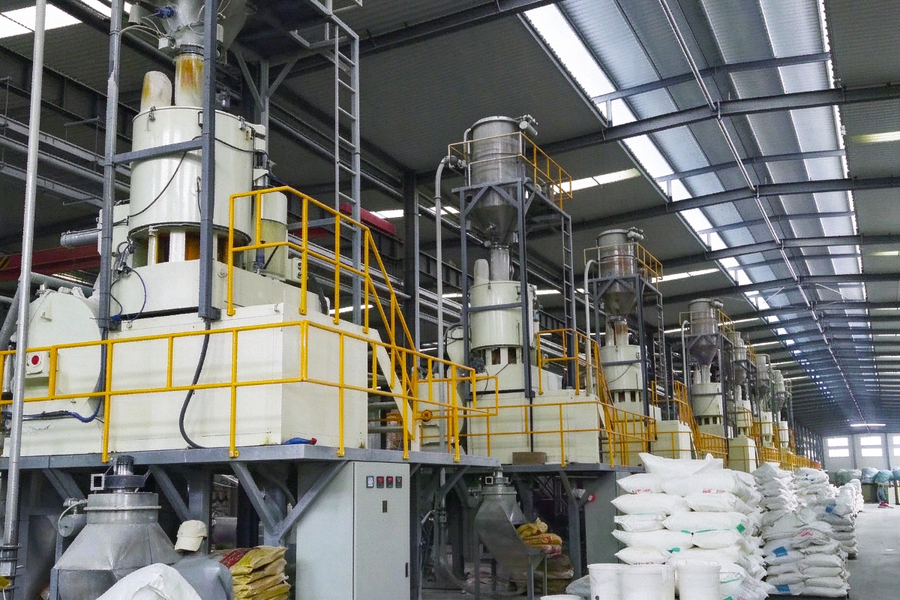
Mixing & Compounding
Mixing & Compounding Weighed raw materials are fed into a high-speed mixer. The hot-mix cycle blends PVC resin, limestone, stabilizers, and processing aids into a homogeneous dry-blend compound. The compound is then cooled in a cold mixer before being transferred to the extrusion hoppers. The mix ratio at this stage determines the final properties of the core. For SPC, the formulation is designed for rigidity and dimensional stability. For LVT, the formulation is adjusted for flexibility and comfort underfoot. Because the compound is prepared in batches and tested before release to production, every extrusion run starts from the same controlled base. This is what keeps the core consistent from one production run to the next.
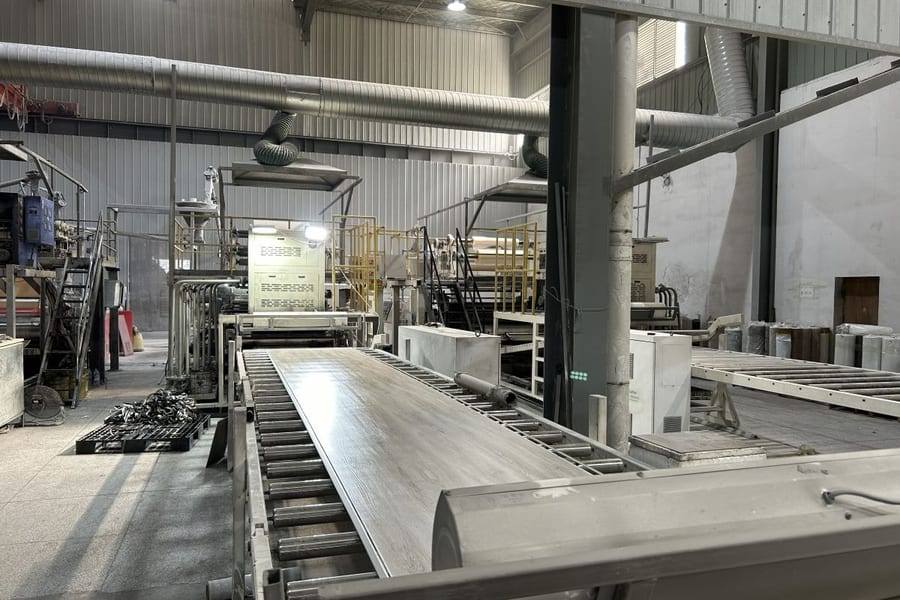
Extrusion
The compounded material is fed into twin-screw extruders, where it is heated and forced through a precision die to form a continuous flat sheet — the SPC or LVT core board. Laser thickness gauges monitor the board in real time to maintain consistent thickness across the run. The extruded board is then cooled on a calender before entering the lamination line. The extrusion line runs continuously, so the core is produced in a single, unbroken sheet rather than in separate batches. This keeps the density and thickness of the board consistent from the start of a run to the end.
Lamination
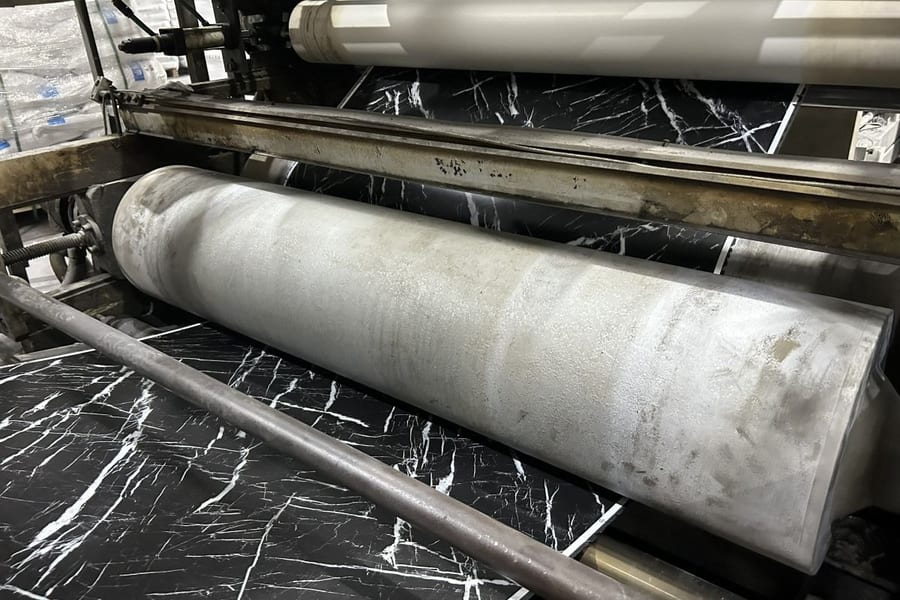
The core board passes through a multi-layer lamination press, where the printed decorative film and the transparent wear layer are thermally bonded to the core under controlled heat and pressure. At the same time, a backing layer is applied to the underside to improve dimensional stability and sound absorption. After bonding, the laminated board is cooled under pressure to prevent warping and to lock in a flat, stable surface before the next stage.
Embossing & UV Coating
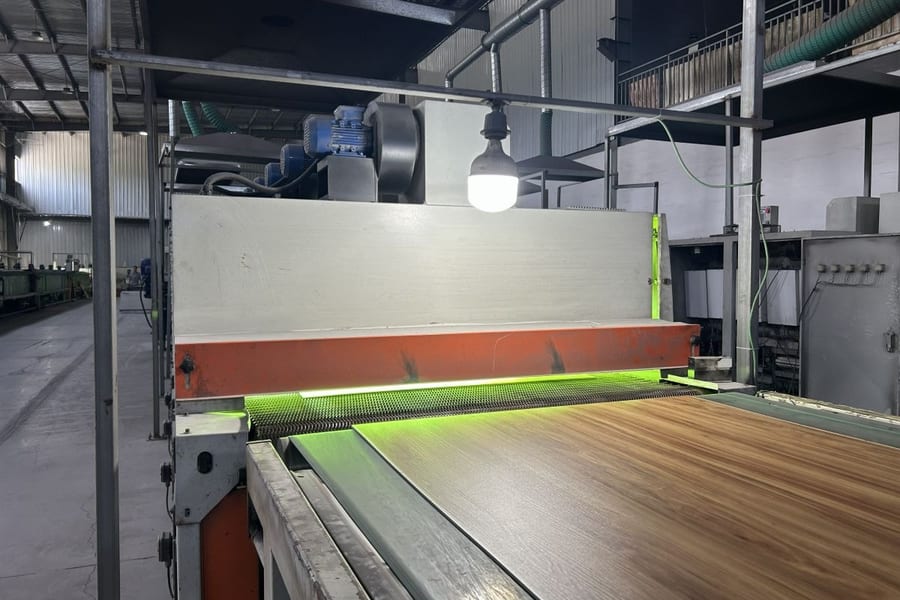
Precision steel rollers engraved with wood-grain or stone textures are aligned with the printed decor on the board below, so the raised texture follows the printed pattern rather than sitting on top of it at random. The result is a surface where the touch and the visual grain match. A UV-cured topcoat is then applied in multiple passes to protect the surface. The coating provides scratch resistance, stain resistance, and control over the final gloss level.
Cutting & Profiling
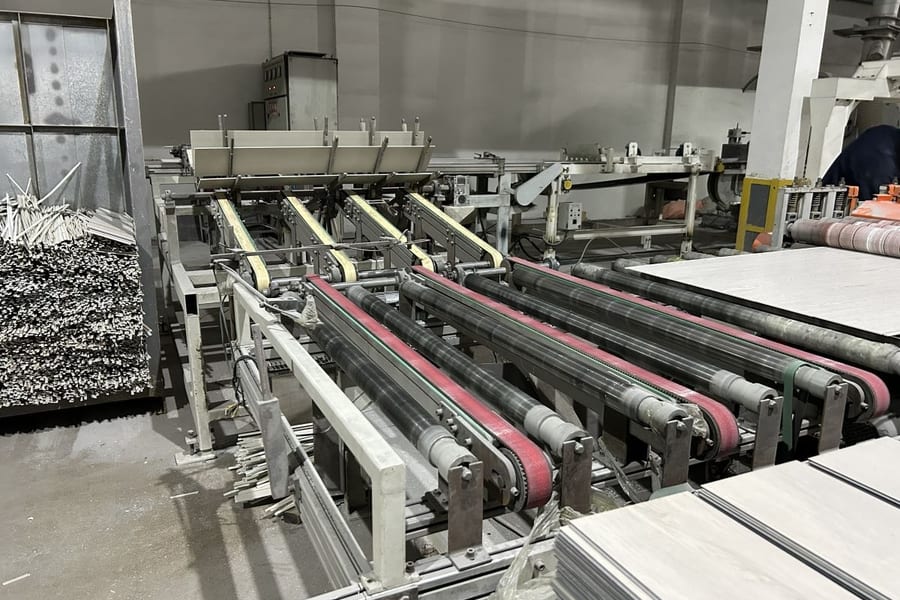
The laminated board is precision-cut to plank or tile dimensions by CNC saws. For click-lock products such as SPC Click, LVT Click, Chevron, and Herringbone, the edges are milled by high-speed CNC profiling machines to form the click system. Profile geometry is checked by automated vision systems on every plank, so any deviation is detected before packing. Chevron and herringbone planks are cut at the required angle to keep the pattern aligned across the floor.
Quality Control
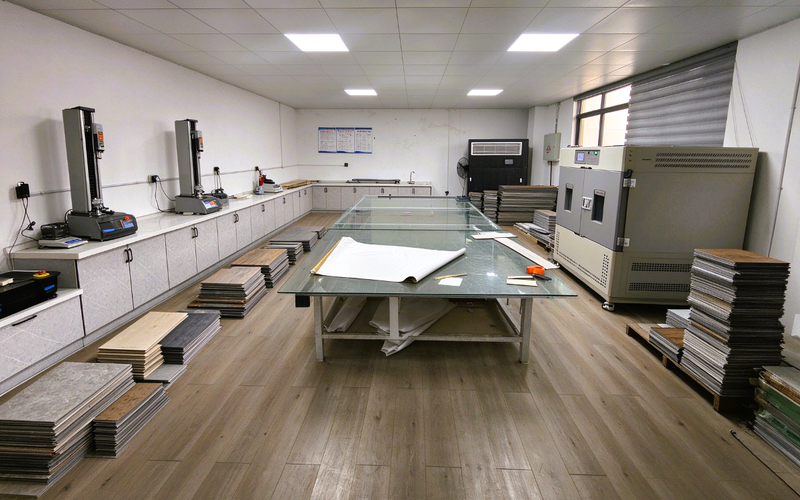
Our QC laboratory performs standardised tests on every production batch. Tests cover dimensional stability, wear resistance, residual indentation, slip resistance, impact resistance, and surface adhesion. All results are logged in our quality management system and retained for traceability. Products that fail any test are quarantined and reviewed before any release decision is made. Test records and retained samples are kept on file for every production batch.

Packaging
Warehouse & Container Loading Finished products are packed in cartons and stacked on pallets. Cartons use neutral packaging by default, or can be printed with the customer's branding on request. Each pallet is protected with hard corner boards, fully wrapped with stretch film, and labeled with shipping marks. Packed pallets are then moved to the finished goods warehouse, where each order is stored together and kept ready for shipment. Before loading, every order is checked against the packing list, then loaded into 20GP containers. We ship to customers in over 50 countries, with loading photos and container seal numbers provided for every shipment.
Want to see the facility in person? We welcome distributor visits year-round.
Book a Factory VisitProduction Process
9-Stage Production Process
Every MGT® plank passes through nine controlled stages before it leaves our facility.
Raw Material Inspection
Incoming PVC resin, limestone, stabilizers, and processing aids are tested and approved before release to production. Formulations are prepared according to each product specification.
Mixing & Compounding
Materials are blended in high-speed mixers through a hot-mix and cold-mix cycle to form a homogeneous dry-blend compound. Consistent quality is verified before the compound is transferred to extrusion.
Extrusion
Twin-screw extruders form the SPC or LVT core into a continuous flat sheet. Laser thickness gauges monitor the board in real time to maintain consistent thickness across the run.
Lamination
Printed decorative film is thermally bonded to the core under controlled heat and pressure. Registration accuracy ensures the decor aligns with the embossed texture applied later.
Embossing
A transparent wear layer is laminated onto the decor film, followed by a UV-cured topcoat applied in multiple passes for scratch and stain resistance.
Cutting & Profiling
Precision steel rollers emboss the surface texture, aligned with the printed decor below. This creates a surface where the touch and the visual grain match.
Quality Inspection
CNC profiling machines mill the click-lock profile on each plank. Automated vision systems verify the profile geometry before the plank moves to the next stage.
Packaging
Standardised tests are performed on every batch: dimensional stability, wear resistance, residual indentation, slip resistance, impact resistance, and surface adhesion. All results are logged in our quality management system.
Warehousing & Dispatch
Products are packed in cartons with full batch traceability, stacked on pallets, and stored in our finished goods warehouse ready for export.
Quality Control
Quality control runs through every stage of production — from incoming raw material to packed, palletized flooring. Our QC and production teams work on the same floor, so issues are caught early, not after shipment.
5+
Stage QC
10+
Production Lines
100%
Batch Inspection
15M+ m²
Annual Capacity

Quality control is at the centre of everything we do. Every production batch is inspected at multiple stages.
Production Consistency
Our 10+ production lines run on standardised settings across all shifts, with in-line measurement at each stage. This keeps thickness, wear layer, and surface finish consistent from batch to batch — order after order.
Waterproof Backing Technology
Closed-cell foam and IXPE backing systems that provide acoustic dampening, thermal insulation, and a complete moisture barrier — eliminating the need for separate underlay in most applications.
Synchronous Wood-Like Technology
Next-generation embossing where the surface depth, direction, and texture are digitally mapped to the printed grain pattern — producing a surface feel close to real wood.
Quality Lab
Every batch is tested for dimensional stability, wear resistance, locking strength, and surface adhesion before release. Test records and retained samples are kept on file for every production batch.
Custom Decor Development
If you have a specific color or pattern in mind, send us a photo or a physical sample. We will work with our film suppliers to develop it, match the decor to be the same as your sample, and produce it for you.
Raw Material Control
We source PVC resin, limestone, and stabilizers from qualified suppliers and test incoming materials before production. Only approved batches enter the line.
Quality Assurance
Quality Control at Every Stage
Every batch is inspected at multiple points — from incoming raw material to finished, packed product.
Incoming Material Inspection
All raw materials are checked before entering production. PVC resin, limestone, stabilizers, and processing aids are tested for particle size, moisture content, and bulk density. Only approved batches are released to the production line.
In-Process Monitoring
Key parameters such as thickness, density, and dimensional stability are monitored during production. In-line measurement systems check the board at each stage, and any deviation is flagged before the next process begins. This keeps output consistent across every production run.
Finished Product Testing
Samples from each batch are tested for dimensional stability, wear resistance, locking strength, and surface adhesion. Tests are carried out in our laboratory using calibrated equipment. Results are recorded and retained for traceability.
Pre-Shipment Inspection
Final visual and functional checks are carried out before loading. Packing, labeling, and pallet condition are verified against the order. Loading photos and container seal numbers are provided for every shipment.
Laboratory Tests
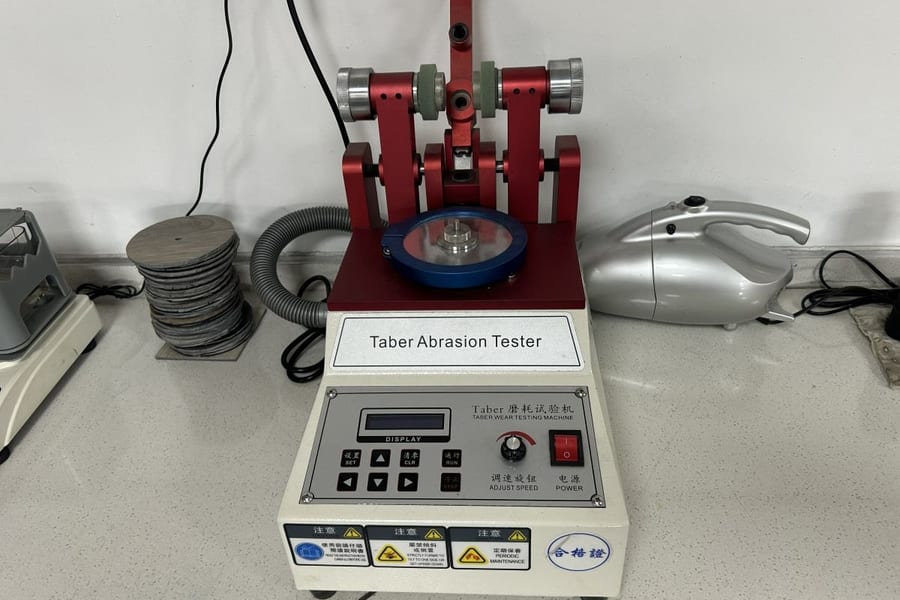
Abrasion resistance
Taber abrasion tester
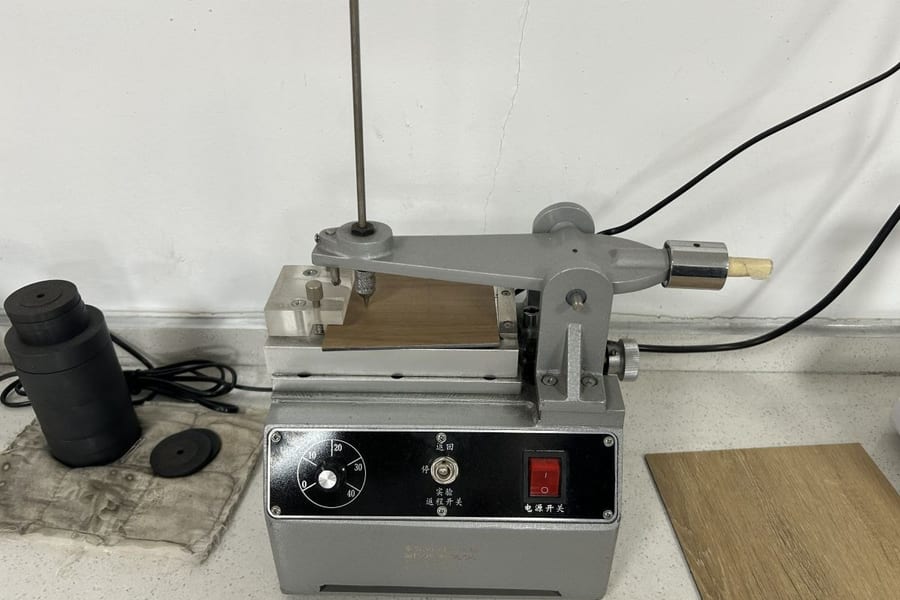
Scratch resistance
Scratch resistance tester
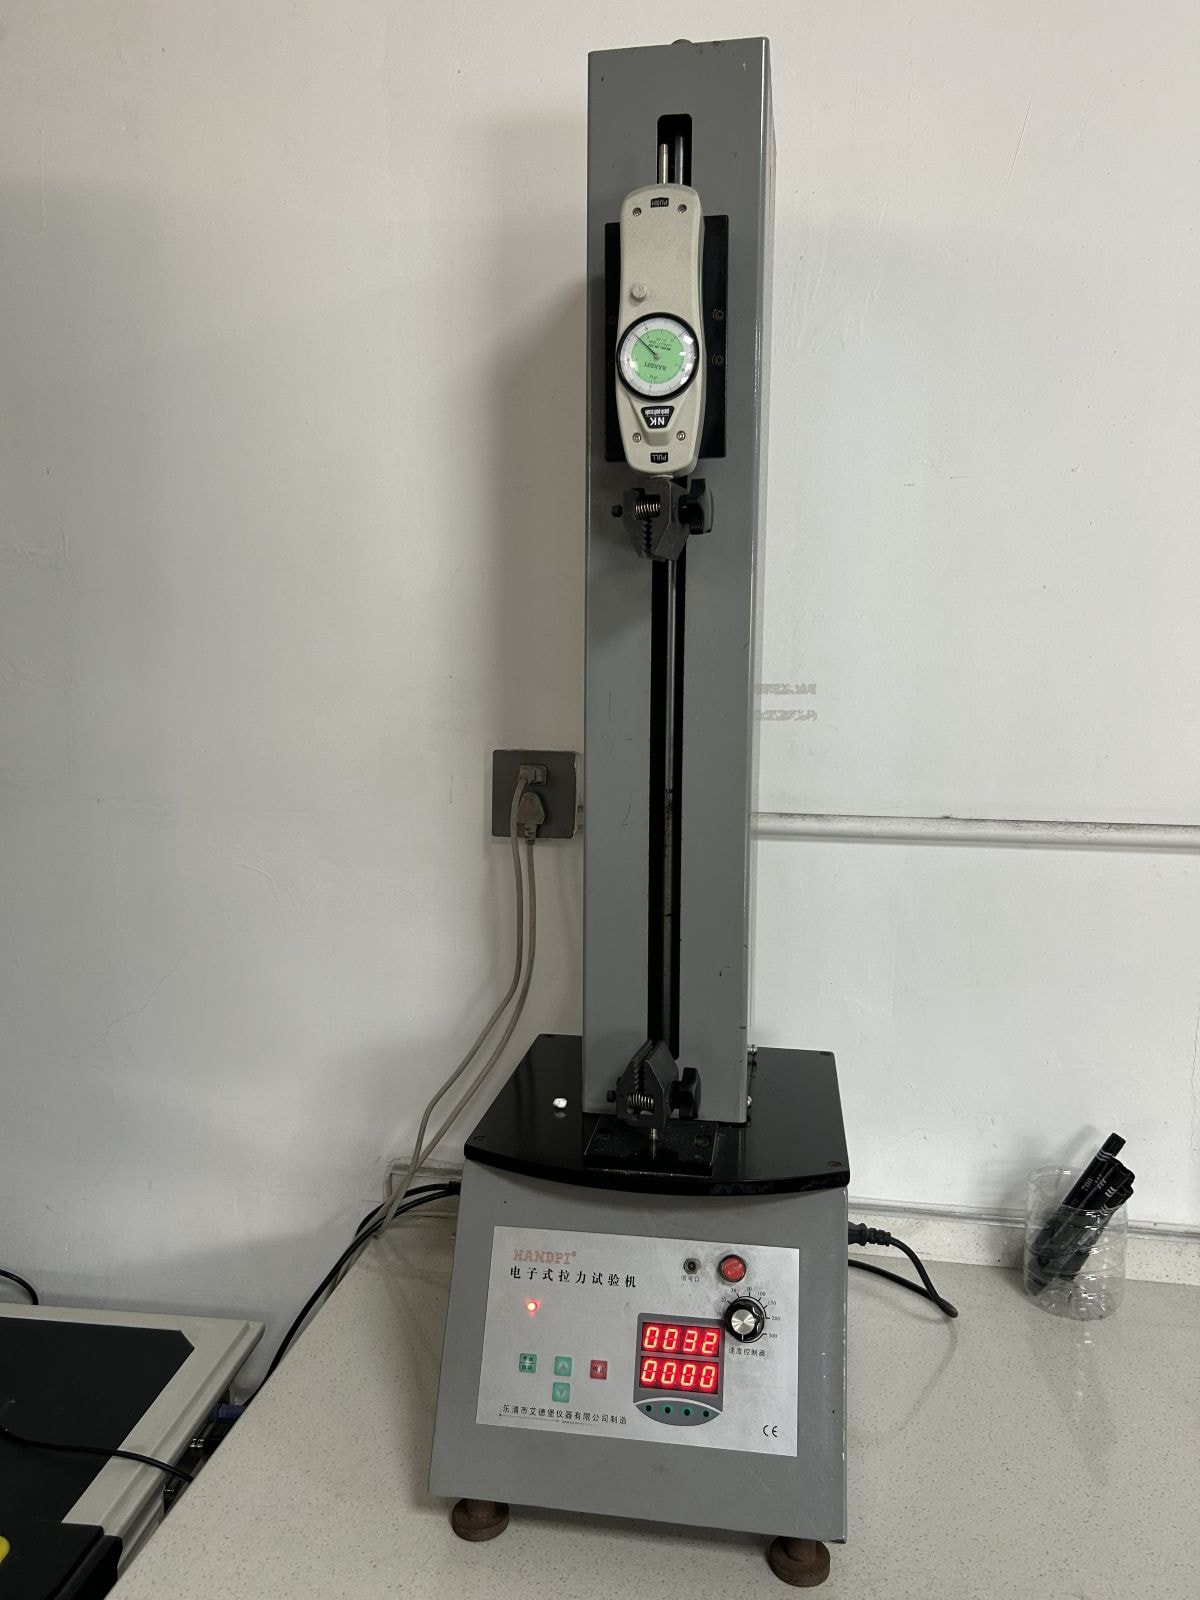
Tear force
Tear force test machine
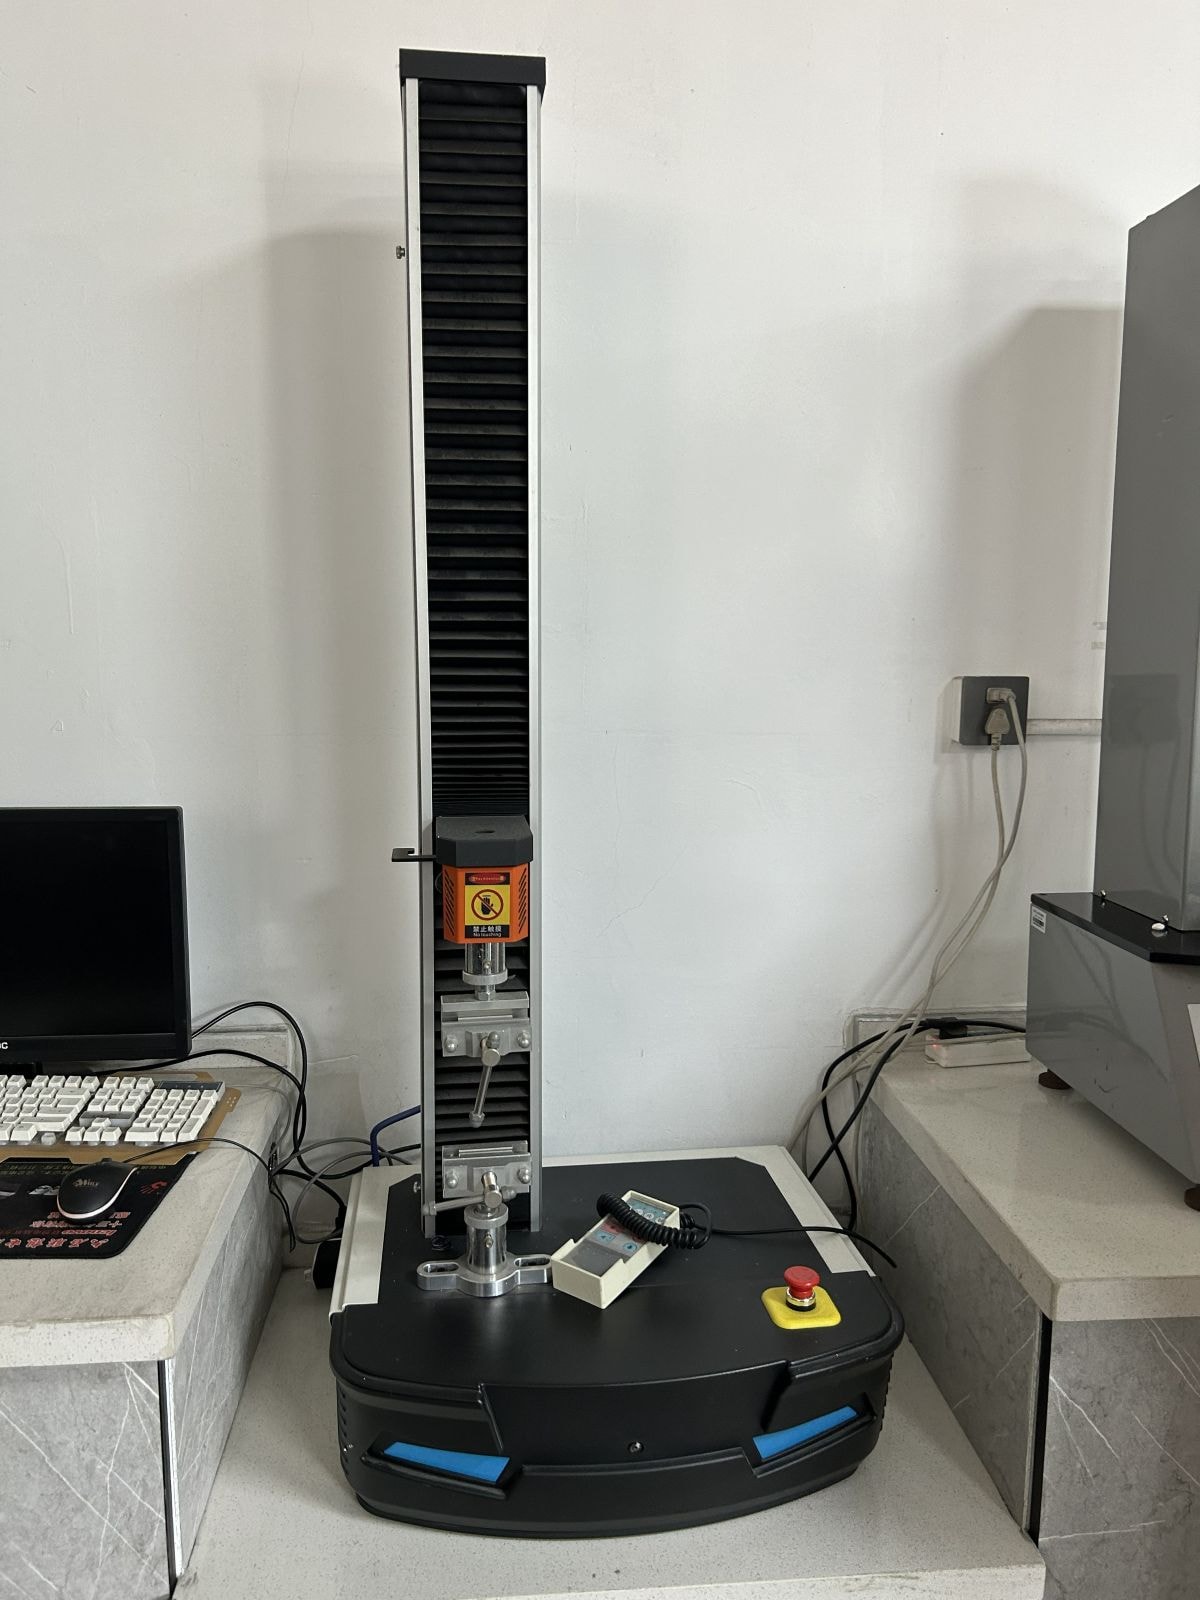
Locking system pull resistance
Locking system pull resistance machine
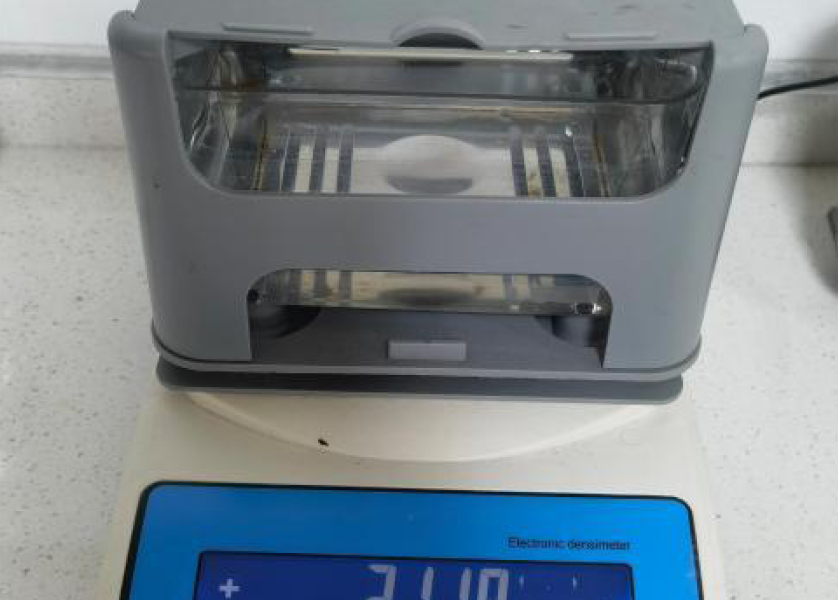
Specific gravity
Electronic hydrometer
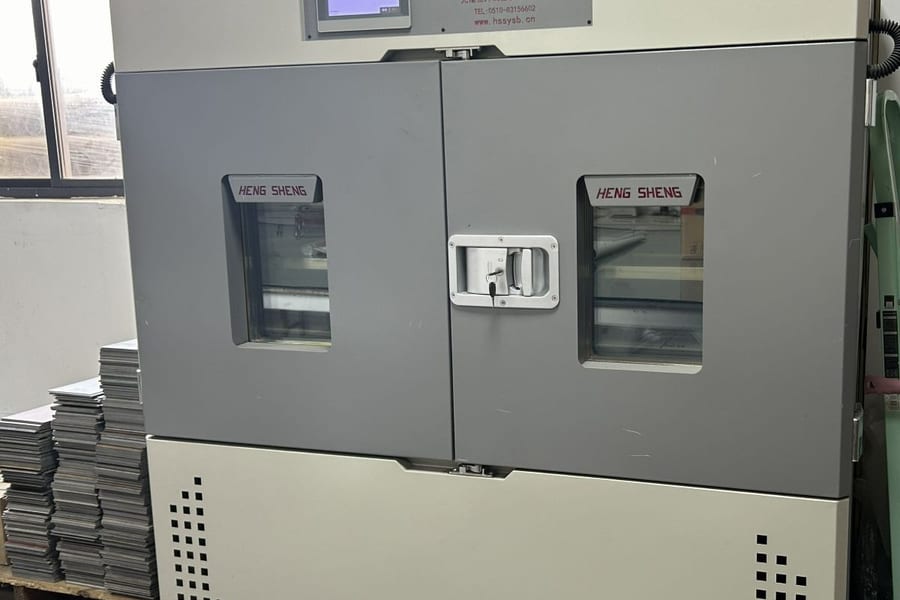
Warping & shrinkage
Oven testing
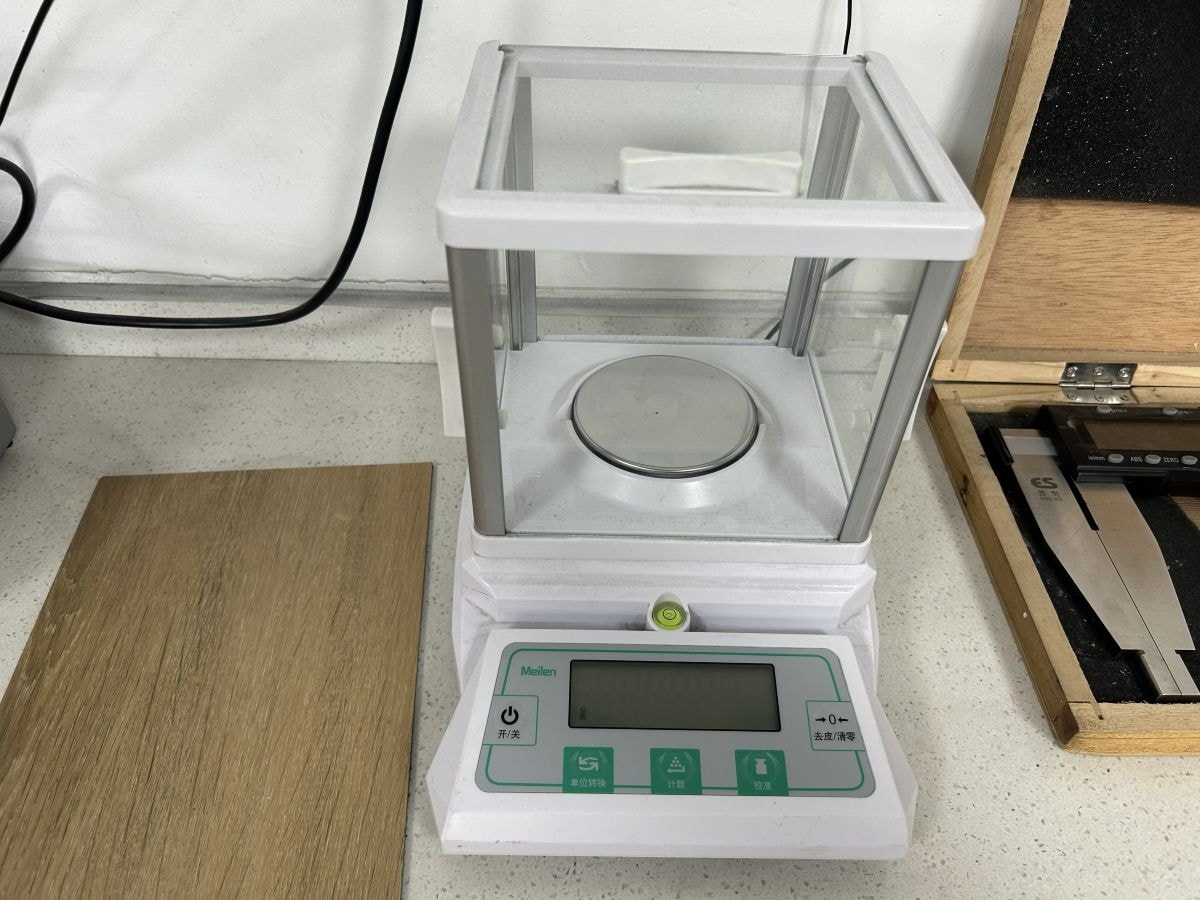
Weight measurement
Electronic balance
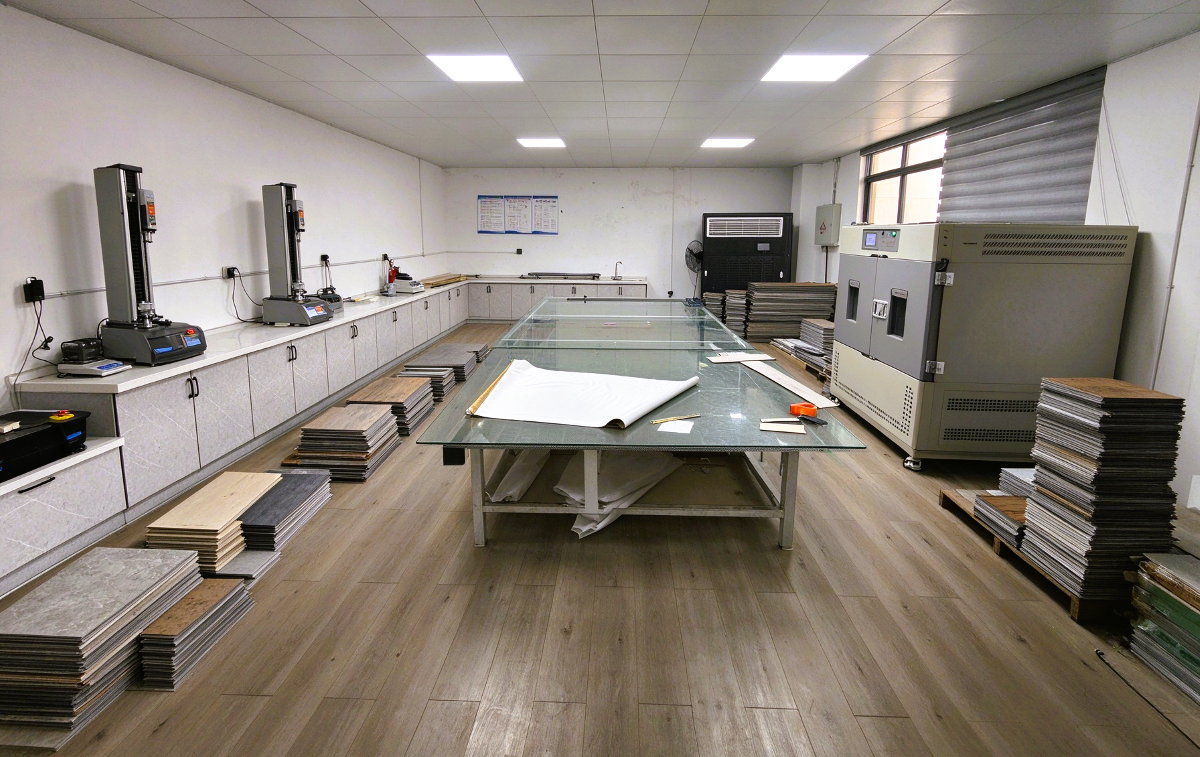
Testing Room
Laboratory for batch testing and quality verification.
Want to see it in person?
We welcome partners to visit us. Our team responds to every enquiry within 24 hours.